

01 – Measurement & Regulation of Air speed in pneumatic product transfer pipe.
Process stability in feeding process while ensuring lowest air speed during dynamic system changes,
02 – Feeding duration definition and process optimization for each Maker.
The PARS program monitors the feeding duration and cycle of the Maker machine and issues a warning alarm to the operator if the pre-defined feeding duration is exceeded within consecutive
03 – Pipe Blockage Prevention and Early Tobacco Choke-up Alarming.
This function aims to minimize Maker downtime caused by 'No Tobacco' issues. If vacuum pressure is detected at the tobacco transfer pipe with low air speed for a certain period,

05 – Minimum pressure presence control allowing to start product transfer.
The objective of this function is also to minimize Maker down time due to Maker «No Tobacco» reason Avoids potential choke up risk in the pipe due to poor capability
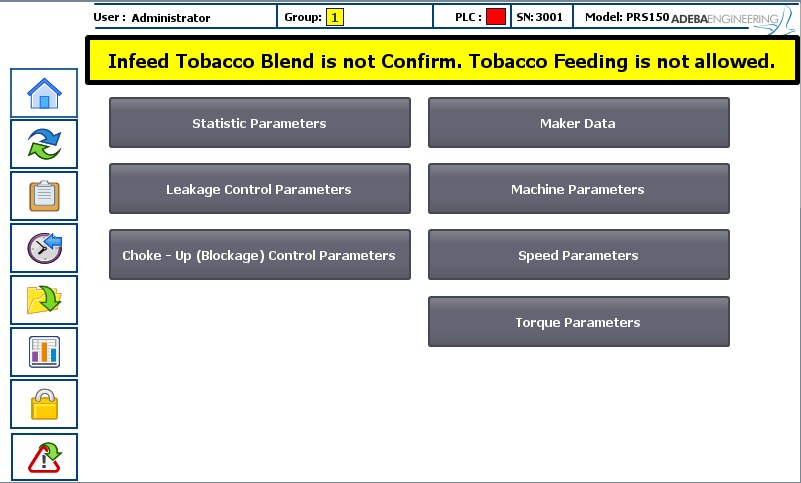
06 – Blend security with advanced automation control.
PARS is designed as bridge in between processes It is able to communicate with Primary Servers as well as Maker operators and eliminates wrong tobacco feeding possibility to Maker.
07 – Recipe management flexibility for individual Blend base air speed adjustment flexibility.
This is to support give flexibility to operators to define different settings possibility for each Tobacco type Option.
08 – Predisposed for Data transfer system adaptation to upper SCADA data collection & monitoring systems.
This is to submit reports and help for easy analyses guideline process improvement studies